
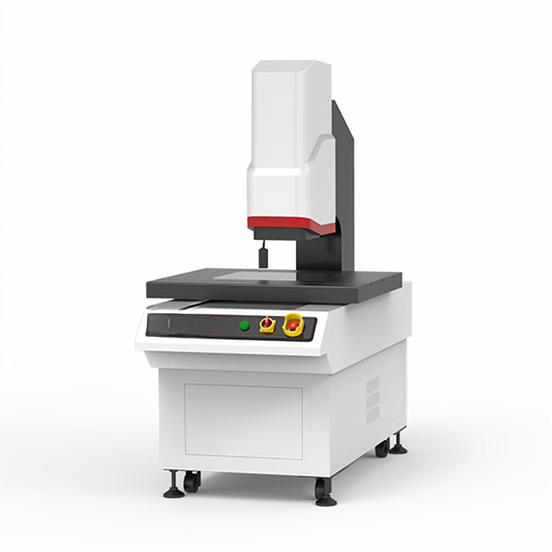
AI Deep Learning Vision System HV-AI
Product Features
Deep-learning inspection
Defect & OCR detection stable in complex scenes
Vision guidance
Robust positioning for robot loading & assembly
Sort & reject
Online sorting with weighing and reject mechanism
Industry packs
Pre-built hardware / food / 3C packs for fast rollout
Deep-learning inspection & recognition
Built-in deep-learning defect detection and OCR recognize scratches, missing parts, misassembly and characters stably under complex backgrounds, cutting false accepts and misses.
Vision positioning & robot guidance
Built on the same geometry core, it provides robust vision positioning and guidance for loading, assembly and pick-and-place automation.
Industry packs for fast rollout
Pre-set hardware, food and 3C inspection packs with configurable models shorten the path from prototype to line.
Technical Specifications
| Parameter | Specification |
|---|---|
| Capability | Defect / OCR / guidance / sorting |
| Camera | Industrial camera (resolution per solution) |
| Inference | Edge / IPC deployment, low latency |
| Models | Configurable DL models + industry packs |
| Interface | Industrial Ethernet / I/O / robot comms |
Can the equipment integrate with my MES or PLC?
Yes, and it is standard capability rather than a paid add-on. The host software provides multiple interfaces: TCP sockets, Modbus TCP and discrete I/O handshaking for PLCs, and REST APIs or direct database access for MES, ERP and QMS. Work orders, serial numbers, measurement results, verdicts and reject reasons can all be exchanged bidirectionally. The process is: agree on the interface and field mapping, commission in a test environment, validate with real work orders, then switch over on site. If the counterpart system only supports file exchange (CSV/XML), polling a shared folder is also supported.
What are the measurement accuracy and repeatability?
One-click flash measuring devices typically achieve micron-level positioning accuracy, but repeatability matters more because it determines whether the equipment can hold your tolerance band reliably. A practical rule is that repeatability should be better than one fifth of the tolerance band, and one tenth for critical characteristics, with margin left for temperature, fixturing and surface condition. Accuracy figures only mean something when tied to measuring range, ambient temperature and calibration method; a single unqualified number is misleading. In the technical agreement we state the accuracy and repeatability for your working conditions and define the acceptance method.
What installation space and power supply does the equipment need?
Four conditions should be confirmed before installation: the machine footprint plus service access, allowing maintenance clearance around the unit; table load capacity and levelness, with precision equipment placed on a separate foundation or vibration-isolated table away from presses and compressors; power, typically single-phase 220V with a stabilized or isolated supply and reliable earthing; and environment, avoiding direct sunlight and air-conditioner drafts because temperature and humidity swings directly affect repeatability. With a formal quotation we provide the installation conditions checklist and a site layout drawing for preparation.
Do I need dedicated fixtures?
It depends on part geometry and locating requirements. Regular, flat, orientation-independent parts usually need only a simple locating block, which is cheap and quick to change over. Irregular or rolling parts, parts needing multi-face measurement, and cases where repeat locating accuracy must approach the equipment's own repeatability call for a dedicated fixture, otherwise locating error eats directly into the measurement margin. Fixtures can be built in-house or designed and manufactured by us; determine this during the trial stage so you do not discover handling problems only after the machine arrives.
Does it support fast changeover between multiple part models? How long does it take?
Yes. Measurement programs are stored as product configuration files, so changeover means calling up the right program, usually taking seconds to tens of seconds depending on whether the fixture changes. The system can store an unlimited number of product programs and call them automatically by work order, barcode or PLC signal, avoiding manual program selection errors. With barcode scanning, an operator simply scans the part or work order to switch both program and acceptance criteria. This is one reason we use a configuration-driven architecture: adding a product requires only a new or adjusted configuration, not a code change.
Which communication protocols are supported (TCP, Modbus, REST)?
We support both shop-floor and IT-level integration. Shop floor: custom TCP socket messages, Modbus TCP (configurable master or slave), discrete I/O handshaking and serial ports (RS232/RS485). System level: RESTful APIs with JSON, direct database access, shared-folder file exchange (CSV/XML) and WebSocket real-time push. If your line uses fieldbuses such as OPC UA or PROFINET, these can be connected through a gateway or middleware, and we provide interface documentation to assist. All interfaces are configuration-driven, so no separate software build is needed per protocol.